

Headquarters and R&D Facility
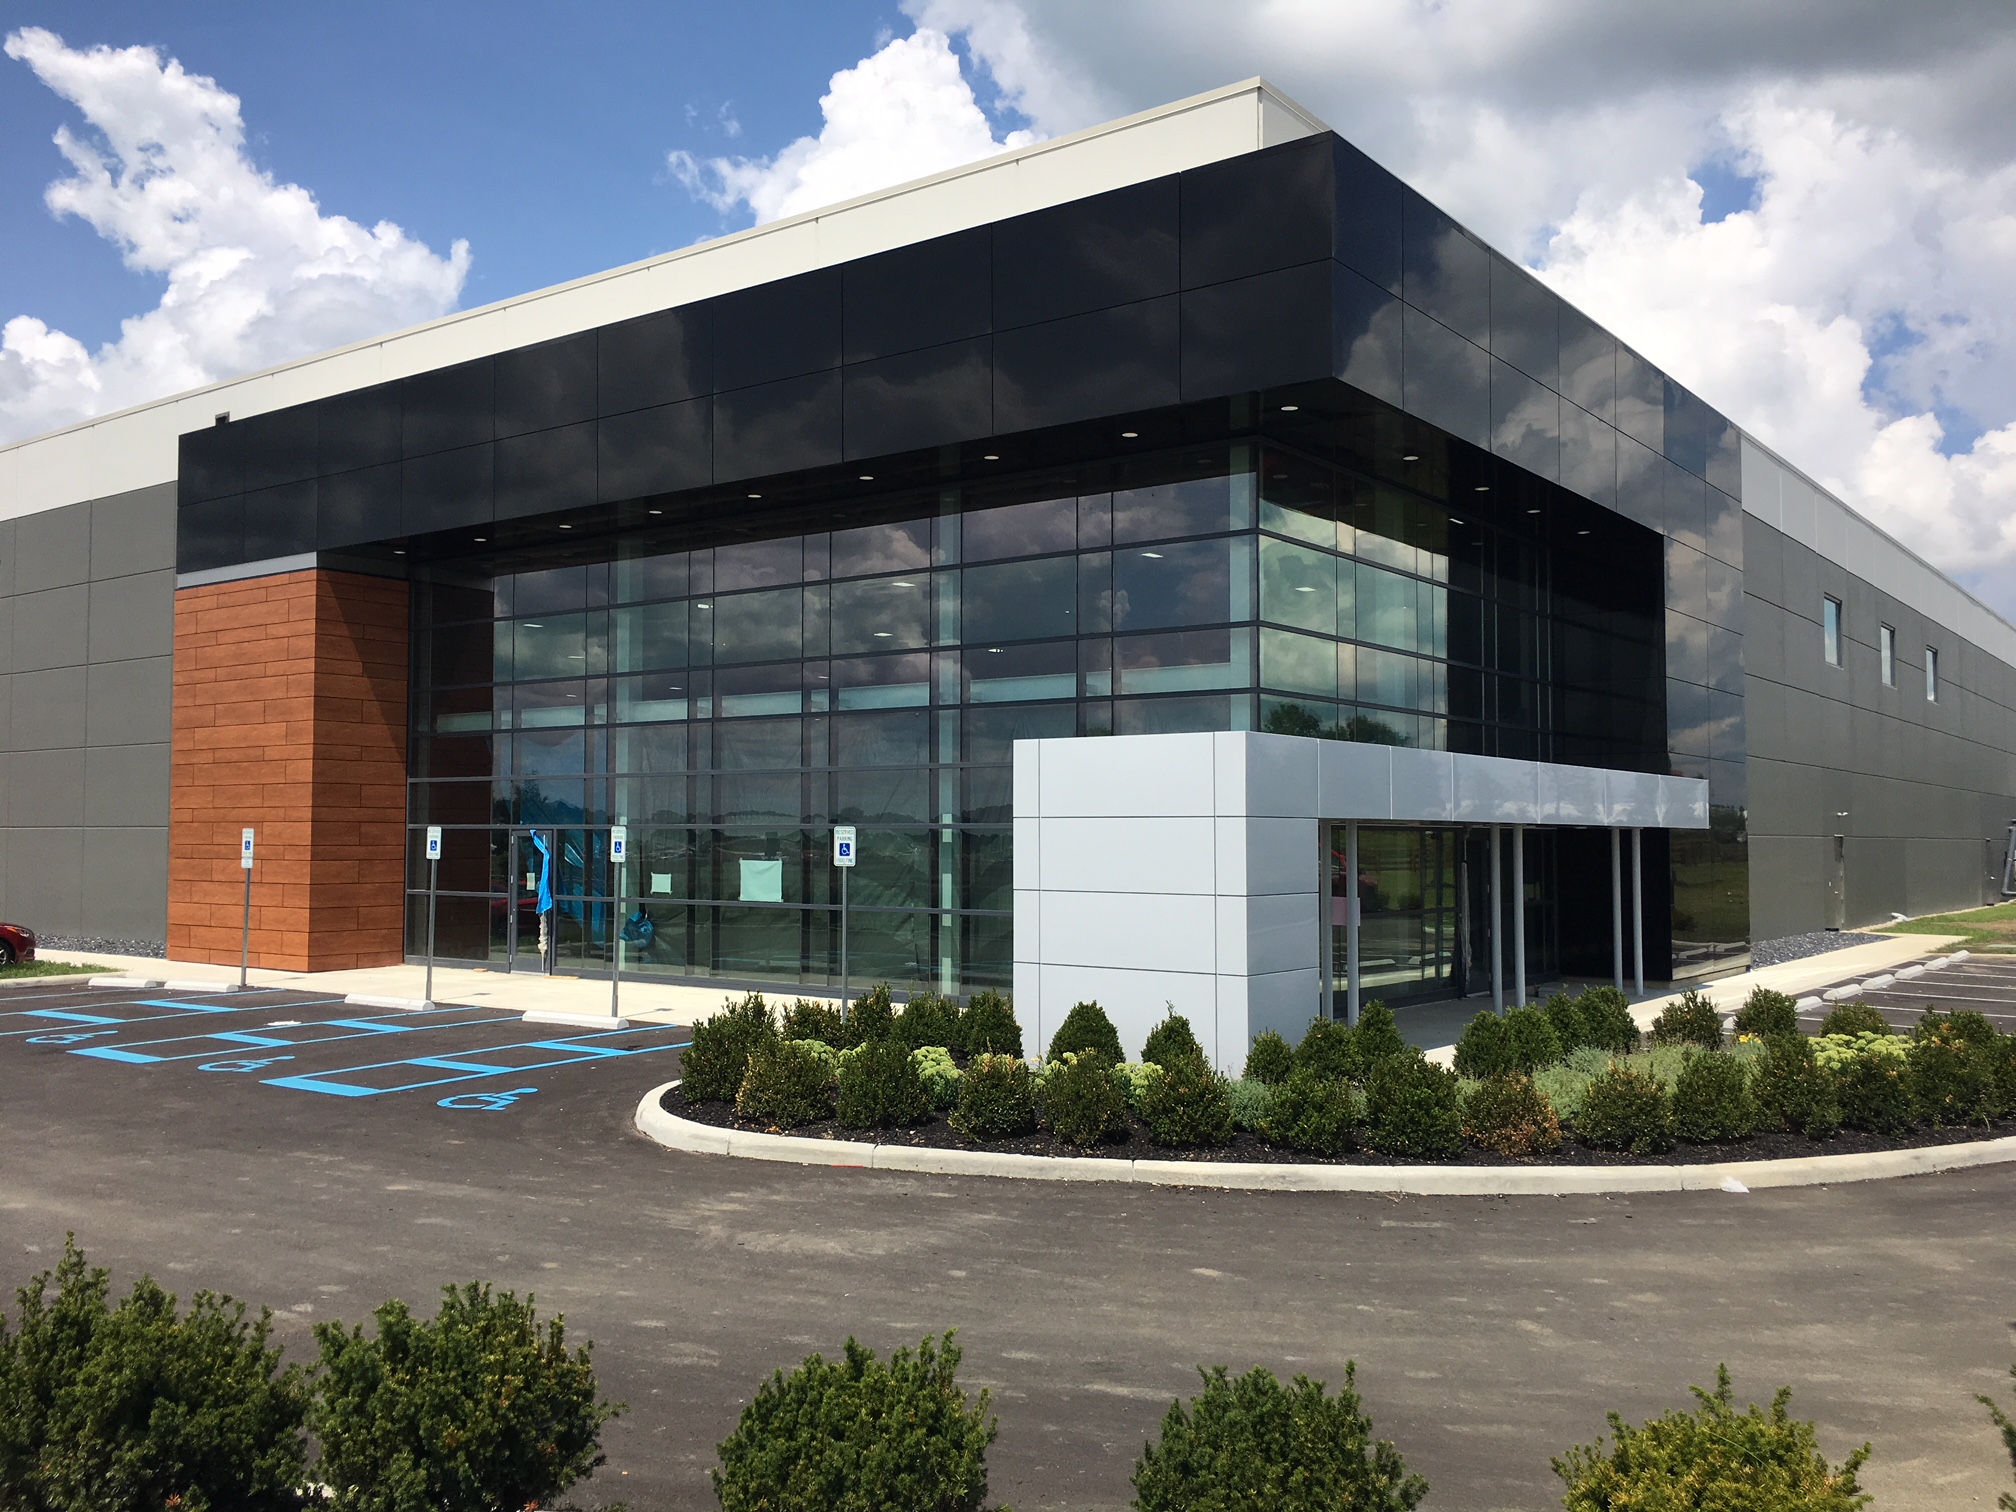
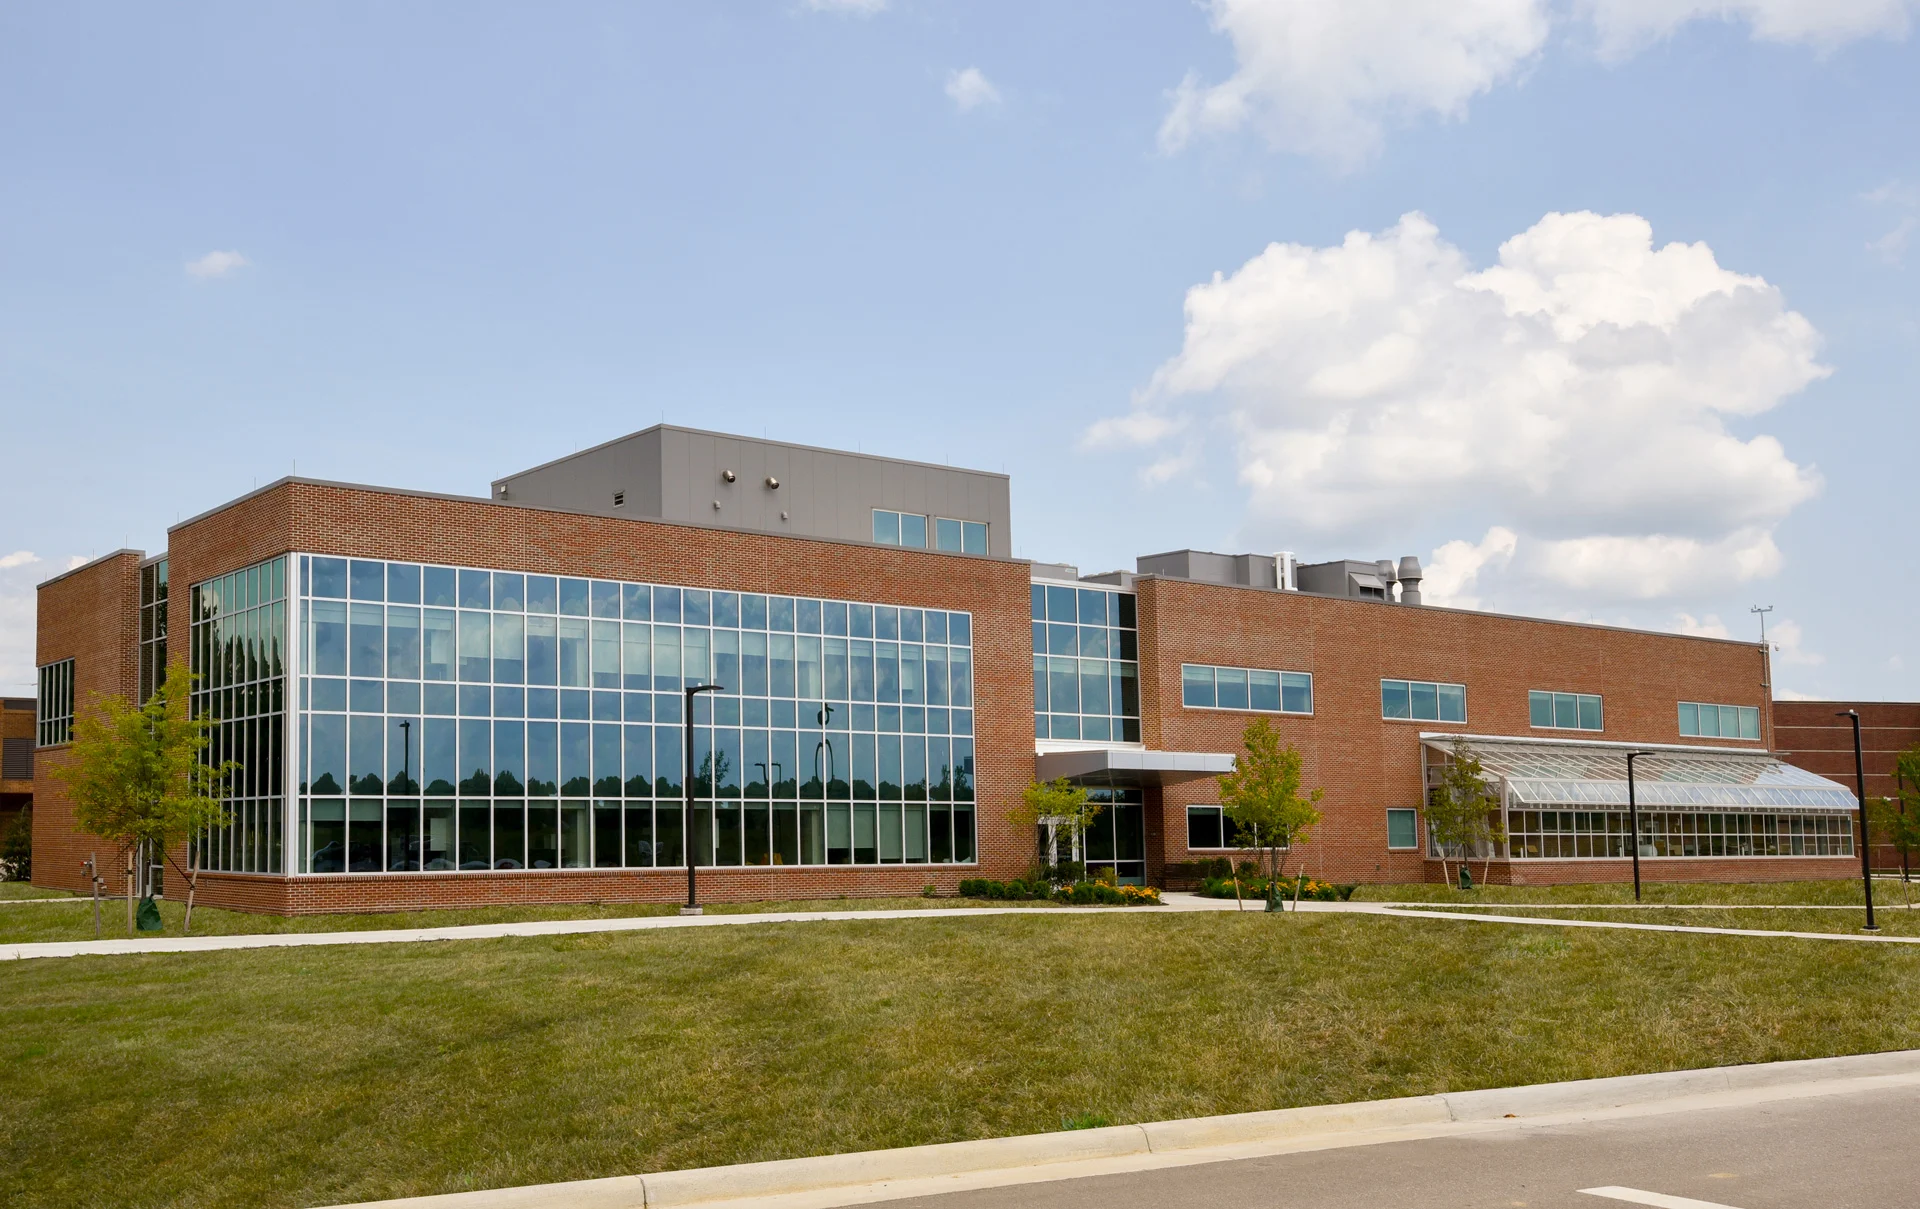
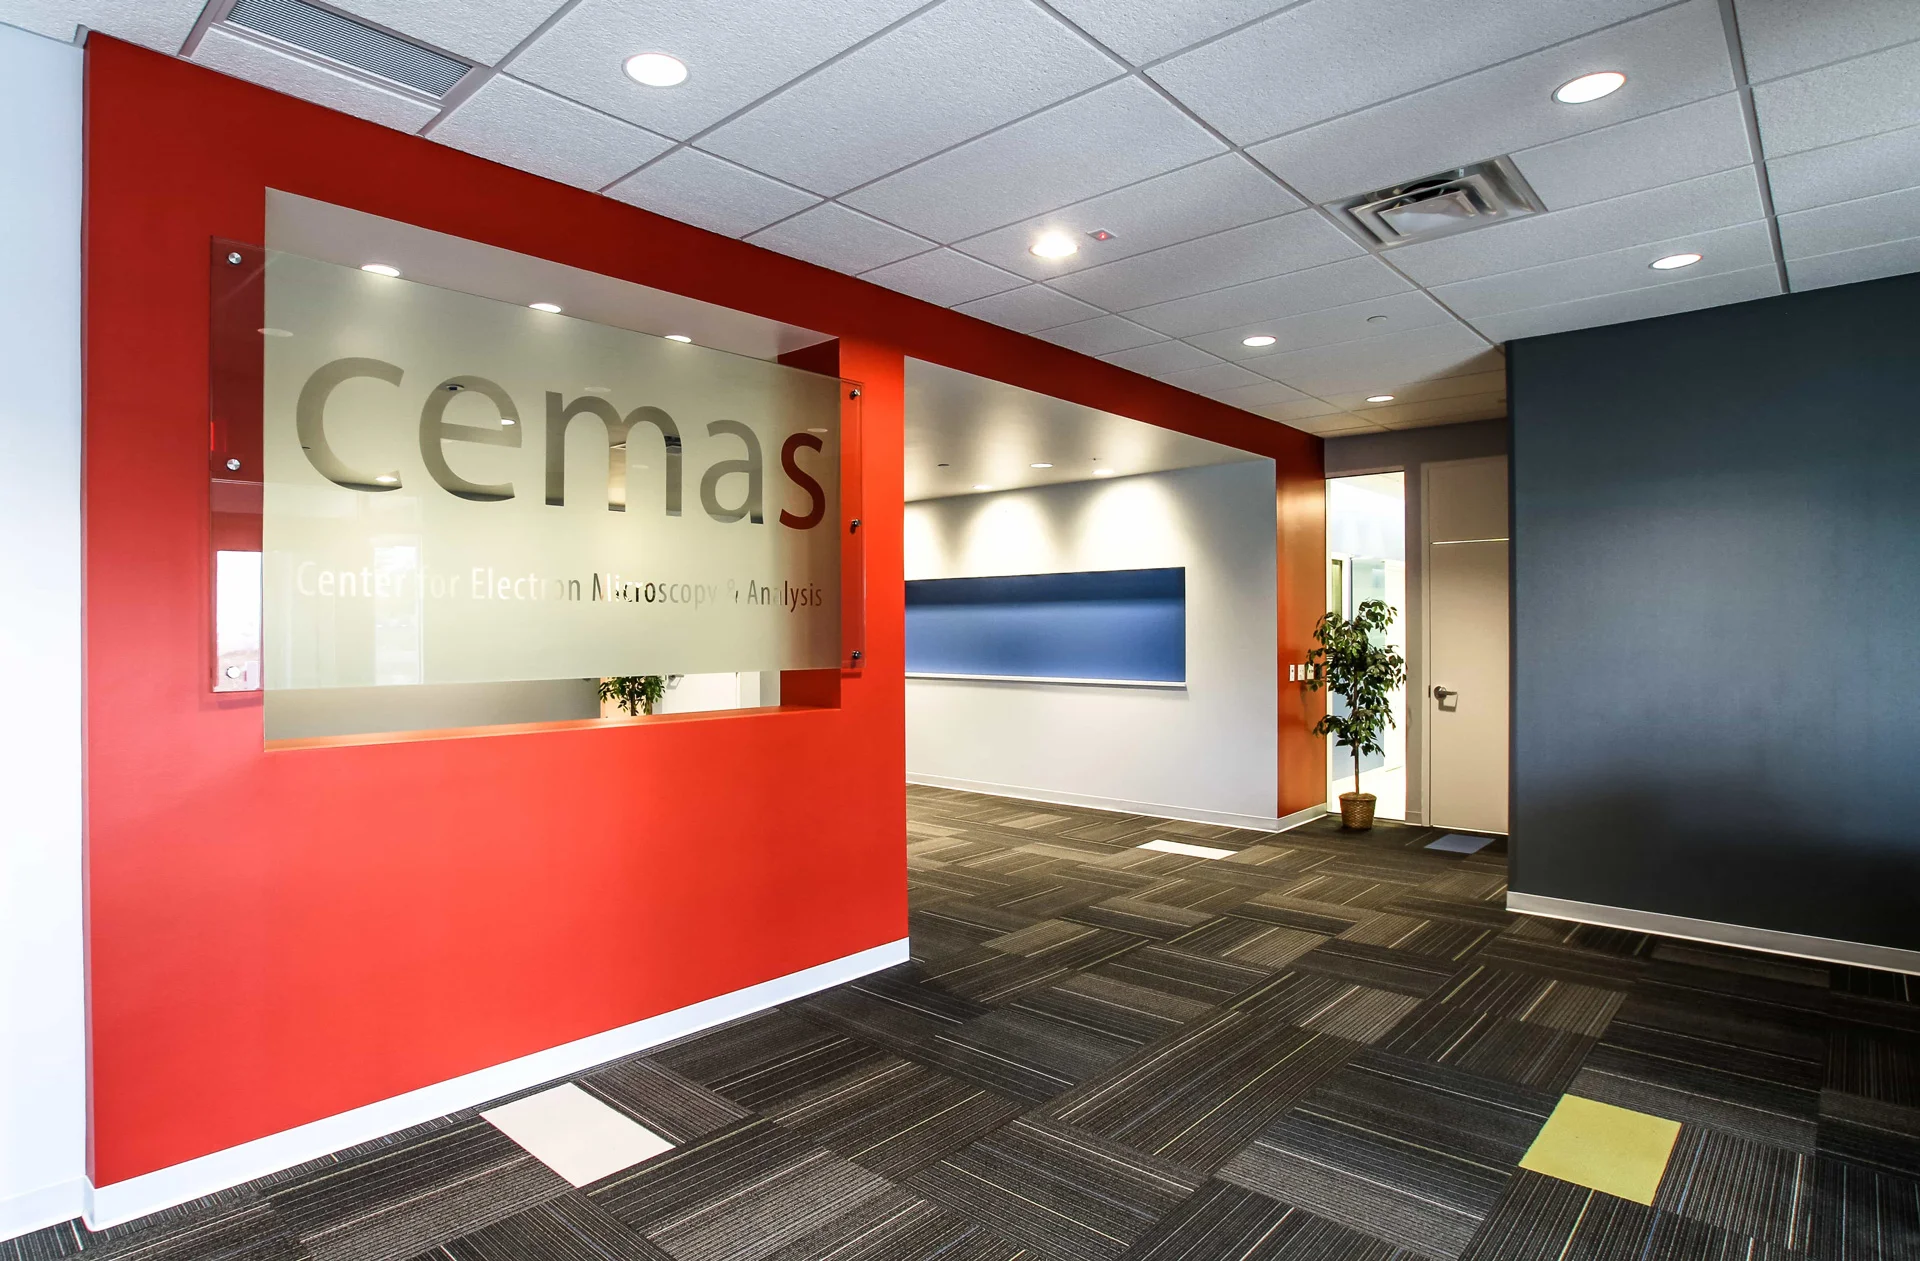
Ruscilli Construction managed the construction of a 20,000sf corporate headquarters and Research and Development facility for PharmaForce, Inc. in Columbus, Ohio. The $3M project provides a modern environment for pharmaceutical research and product development and includes administrative offices alongside specialized laboratory spaces. The facility incorporates Analytical Wet Chemistry, Microbiology, and High Potency Compounding laboratories designed to support the development of new pharmaceutical drugs and formulation testing within a controlled laboratory setting.
Sterile Manufacturing Facility
The PharmaForce Sterile Manufacturing Facility produces sterile solutions and suspensions for ophthalmic, parenteral, and other injectable products using aseptic liquid processing and terminal sterilization methods. The project involved refurbishing and sterilizing an existing 39,000sf building to accommodate approximately 8,000sf of in process office space and 31,000sf of manufacturing and support functions. The manufacturing area includes a 4,000sf classified sterile core featuring Class 10,000 and Class 100 cleanroom environments. The facility was designed to meet current regulatory requirements for process water production, aseptic filling, compounding, dispensing, sterilization, inspection, labeling, packaging, and metrology, with supporting administrative and technical offices for production and quality control operations.
New Albany Office/Lab
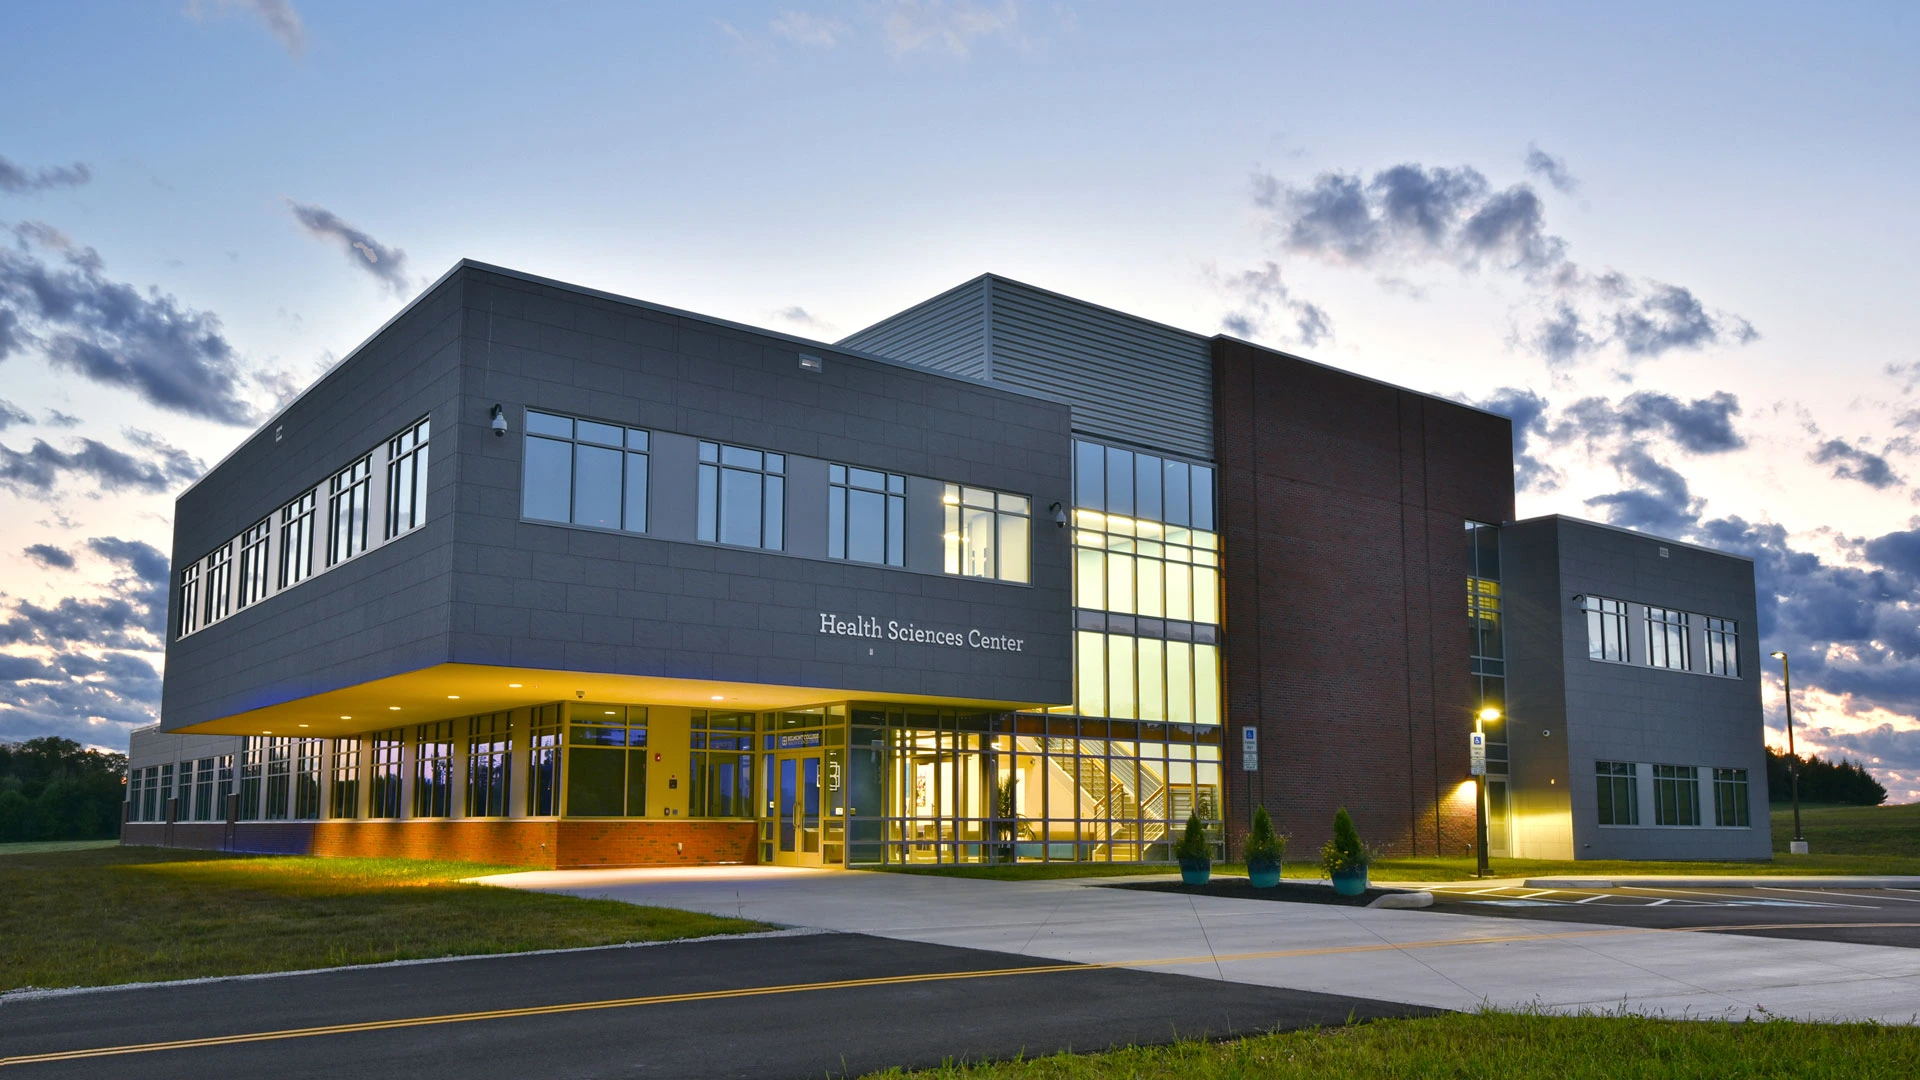
Ruscilli delivered a campus style corporate office, research and development, and process manufacturing facility for PharmaForce, Inc. in New Albany, Ohio. This FDA approved facility includes Analytical Wet Chemistry and Microbiology laboratories, high potency compounding rooms, and clean manufacturing spaces for the production of parenteral and ophthalmic solutions and suspensions utilizing aseptic processing, lyophilization, and terminal sterilization. The building is supported by Class 10,000 and Class 100 cleanrooms, reverse osmosis water purification systems, aseptic filling and compounding suites, dispensing, sterilization, inspection, labeling, packaging, and metrology functions. The facility also incorporates sustainable design features that enhance ventilation, daylighting, landscaping, and bio swales as part of an integrated site approach.